
Rivet spinners?
-
I have such a tool for Motorcycle chains. It´s designed for hollow steel rivets, but it should be able to deform a brass pin easily.
I would be afraid that it might deform (squash) the hle pin instead of forming a head/peen as tere is no "die" to form a rivet head.
The Cahin links have solid pins with hollow ends that gett expanded by the riveting tool and i imagine it to be the same with those chainsaw rivet spinners.
-
There is a vid on youtube doing it with "whole" rivets as the ones in the alox model, a bit larger though. Let me see if I can find it!
chainsawbars.co.uk - breaking and mending a chainsaw chain
and
Cheers!
-
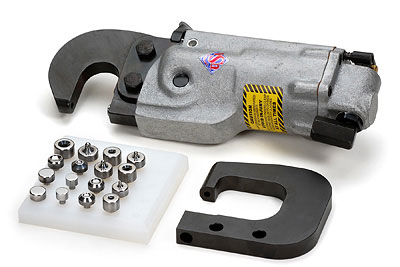
I think those are steel rivets? On brass I think it would just compress the inside portion and bend it, which why you really need something that hits the head repeatedly. I looked into making a peener machine and what I decided was the best approach was borrowing rivetting tools and dies from the aircraft industry. What they use to rivet planes together has dies just like what we'd want, but would run about 300-400 to build something.
Something like this with custom dies for 3mm would do it.
-
What about steel hallow rivets as Lowtech mentions? Those would be ever cooler, and strong enough?
2x 3mm and 1x 2.5mm hollow rivets would be pretty groovy, and open up some interesting lanyard possibilities.
Maybe PTR has some ideas, from what I gather he was/is in the aerospace industry. His trip to Middle Earth is a few more days I believe.
-
Once you go hollow you dont even need a spinner then. All you need is a flaring tool, so there is no peening even needed. I have some some hollow steel 1/8 inch steel pins that Im going to use for this, but havent tried yet. I have flared Ti hollow pins and those were easy enough.
-
Well here are a couple winners for the required metric (or close enough) tubes:
3.0 and 2.2 OD tubes:
3.0 tubes: http://www.microgroup.com/Products/StockTubing/metric_tubing.asp
~2.5 tubes:
Actually there is a whole truck load on Amazon in 304 and 316- a very suitable corrosion resistant grades of SS AFAICT:
http://www.amazonsupply.com/metal-tubing/s/16414261
Cool stuff in general:
-
Im happy doing the screws on 93 mods, but on cadets I dont love them. Very hard to get just right. Id be interested in trying some 2.2mm hollow pins on cadets for sure.

-
This page seems to have some interesting info on flaring tools, I can't say that I know much about them:
37 degrees seems to be the correct angle for SS, the other standard (45 degrees) is said to split the steel.
From a practical standpoint which types of tools would be proper for flaring on an alox sak?
-
Since I'm not planning on doing it I thought I would share my idea. It's quite simple but should be effective. A hammer drill mounted in a drill press like fixture. Then make a bottom die to hold the pin. Install parts and slowly use the hammer drill. This is almost identical to the way Vic does it. It's a special die on a certain angle which I'll explain. The die is 3/6 degrees on a orbiting motion an eccentric. So it rotates and spins and the same time. If you want to do the opposite side all you do is replace the lower die with a drill chuck and do the same operation to have to starting end.
-
I just ground a point on some steel rod then polished it to make a flare tool. I didnt measure the angle at all but it worked ok. Or I got lucky. It was just one rivet. But if you think about it, the end doesnt have to flare out too much to lock the scale on. Id probably do some experimenting before trying it on a proper mod.
-
@tattoosteve99 said:
Since I'm not planning on doing it I thought I would share my idea. It's quite simple but should be effective. A hammer drill mounted in a drill press like fixture. Then make a bottom die to hold the pin. Install parts and slowly use the hammer drill. This is almost identical to the way Vic does it. It's a special die on a certain angle which I'll explain. The die is 3/6 degrees on a orbiting motion an eccentric. So it rotates and spins and the same time. If you want to do the opposite side all you do is replace the lower die with a drill chuck and do the same operation to have to starting end.I bought a hammer drill with the idea of trying something like that, but I figured Id have to get some special dies made to make it work?
-
Since I'm not planning on doing it I thought I would share my idea. It's quite simple but should be effective. A hammer drill mounted in a drill press like fixture. Then make a bottom die to hold the pin. Install parts and slowly use the hammer drill. This is almost identical to the way Vic does it. It's a special die on a certain angle which I'll explain. The die is 3/6 degrees on a orbiting motion an eccentric. So it rotates and spins and the same time. If you want to do the opposite side all you do is replace the lower die with a drill chuck and do the same operation to have to starting end.
I bought a hammer drill with the idea of trying something like that, but I figured Id have to get some special dies made to make it work?
Yeah but still cheaper than a $40k riveter




Hello! It looks like you're interested in this conversation, but you don't have an account yet.
Getting fed up of having to scroll through the same posts each visit? When you register for an account, you'll always come back to exactly where you were before, and choose to be notified of new replies (either via email, or push notification). You'll also be able to save bookmarks and upvote posts to show your appreciation to other community members.
With your input, this post could be even better 💗
Register Login


