
And so it begins.... (My adventures into Alox!)
-
-
Good work... I've been sitting on my hands about doing exactly that for a long time... it got knocked up a notch last week when I cut my finger when the blade on my Electrician folded on me.
I will be
 with much interest...
and not just to see how you work out the geometry so I don't have to
-
Just a prototype for now but if it works I'll build it into a complete mod. Just going to try with a stock blade to start and Im rearranging the layers to the blade is in the front layer, and you will push with the right thumb to unlock. Opposite to how the current Vic 111mm works.
Im not sure if I will be able to have a tool with the blade or not. You know how the blade on a standard pioneer is bent so far it actually sits into the space of the liner.. well this needs a full liner so I dont think it will work. So it might be a solo spring blade layer, then the rest of the tools.
-
Hmm, very interesting! JR
-
Im thinking of a layout like this...
From back to front.
- Back scale
- Can opener / bottle opener layer
- Normal shaped Ti liner
- Scissors
- Locking liner
- Blade
- Front scale
-
-
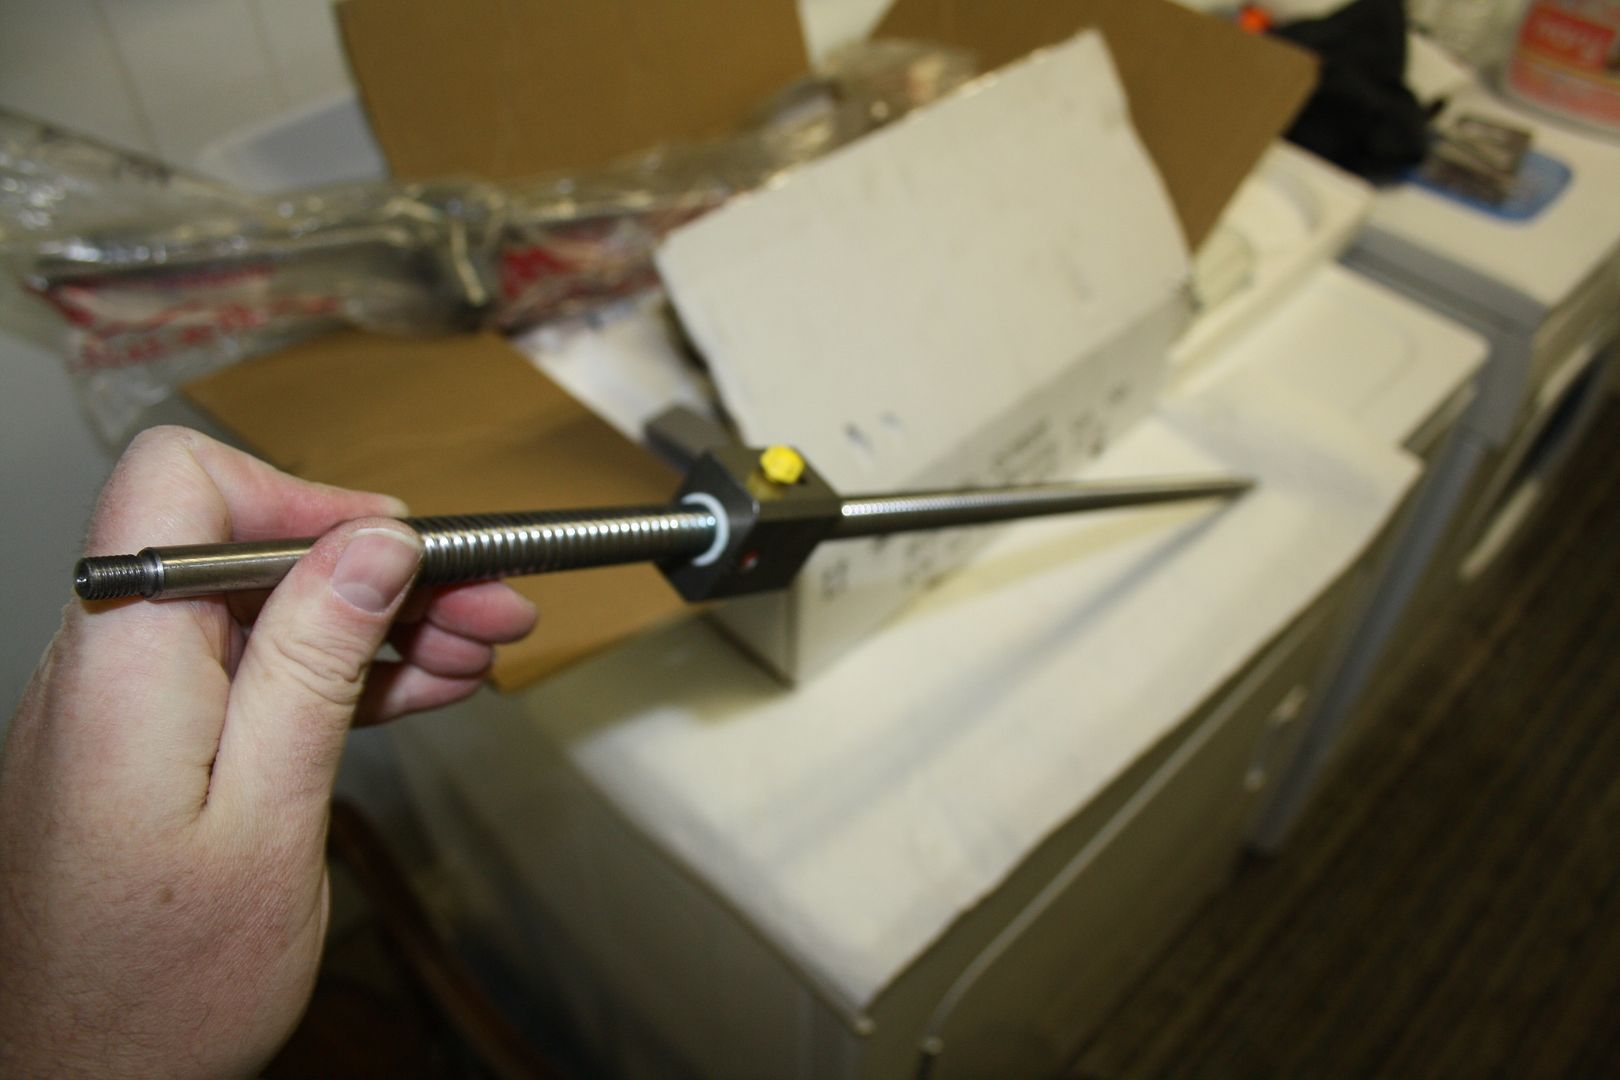
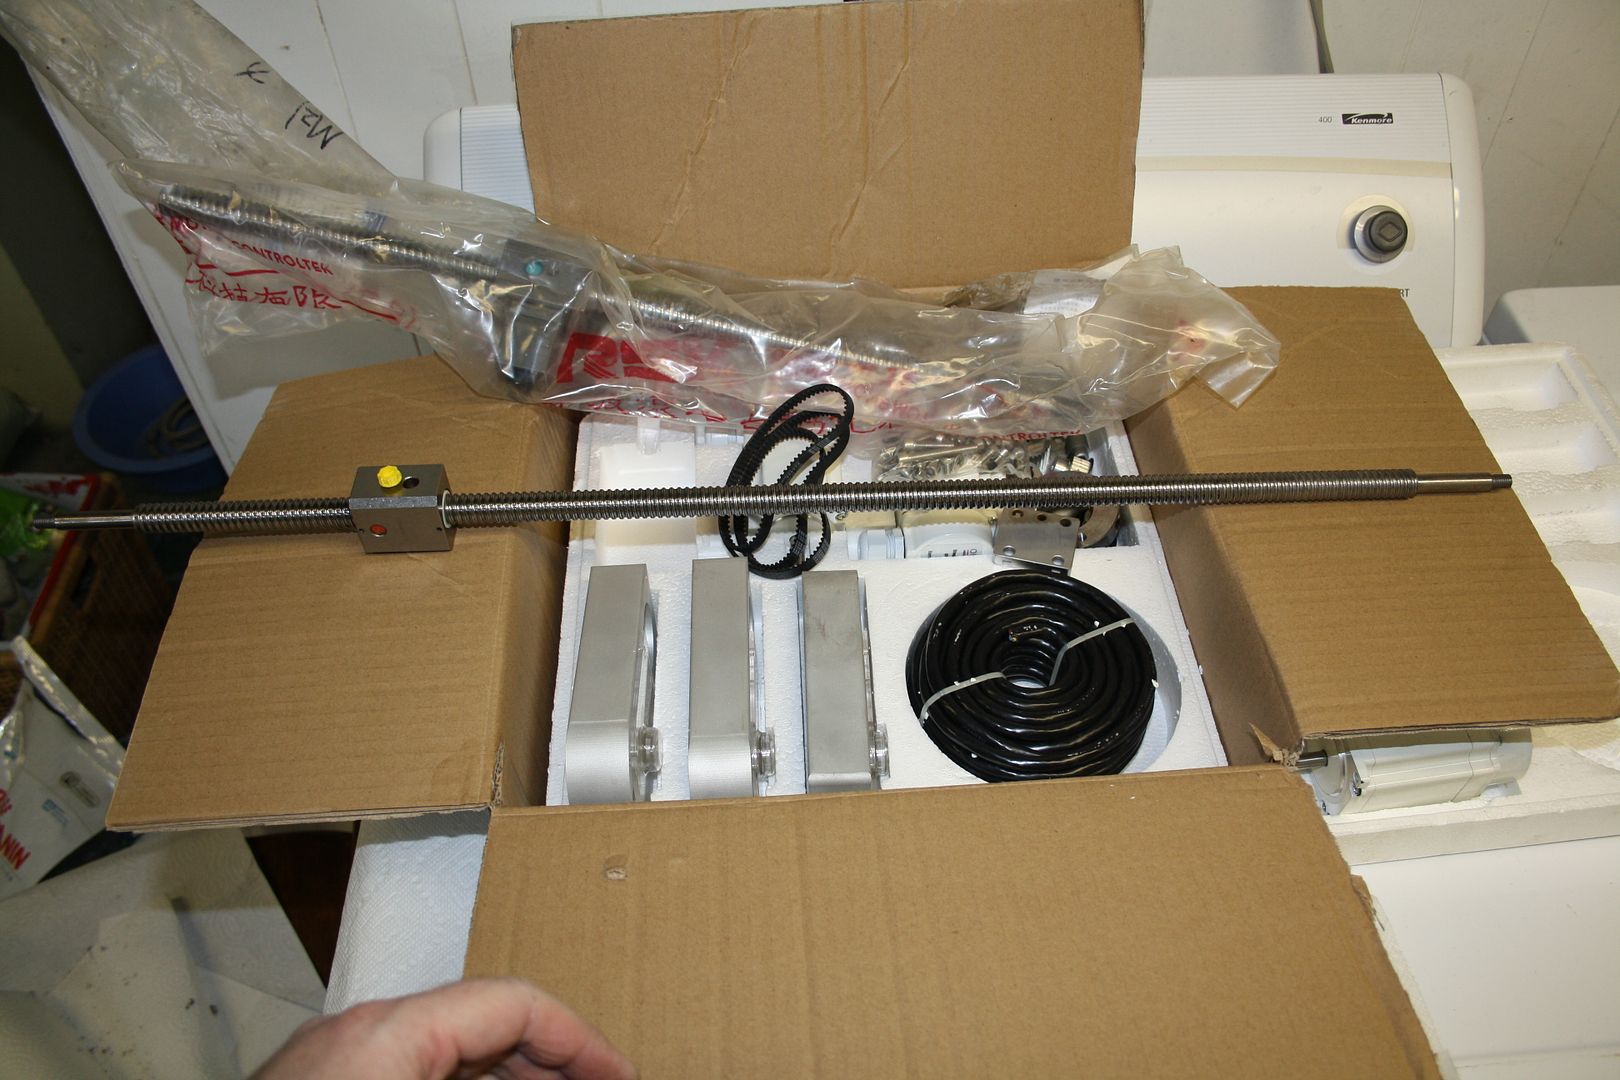
Well my CNC retrofit kit came today finally! :D
Now I just have to figure out how to get it all installed, and pick up a driver board.. flood coolant tank and pump.. and a computer to run it.. learn CAD better.. :D
Hopeful by summer I'll get this all sorted or maybe sooner but its COLD in my shop right now.
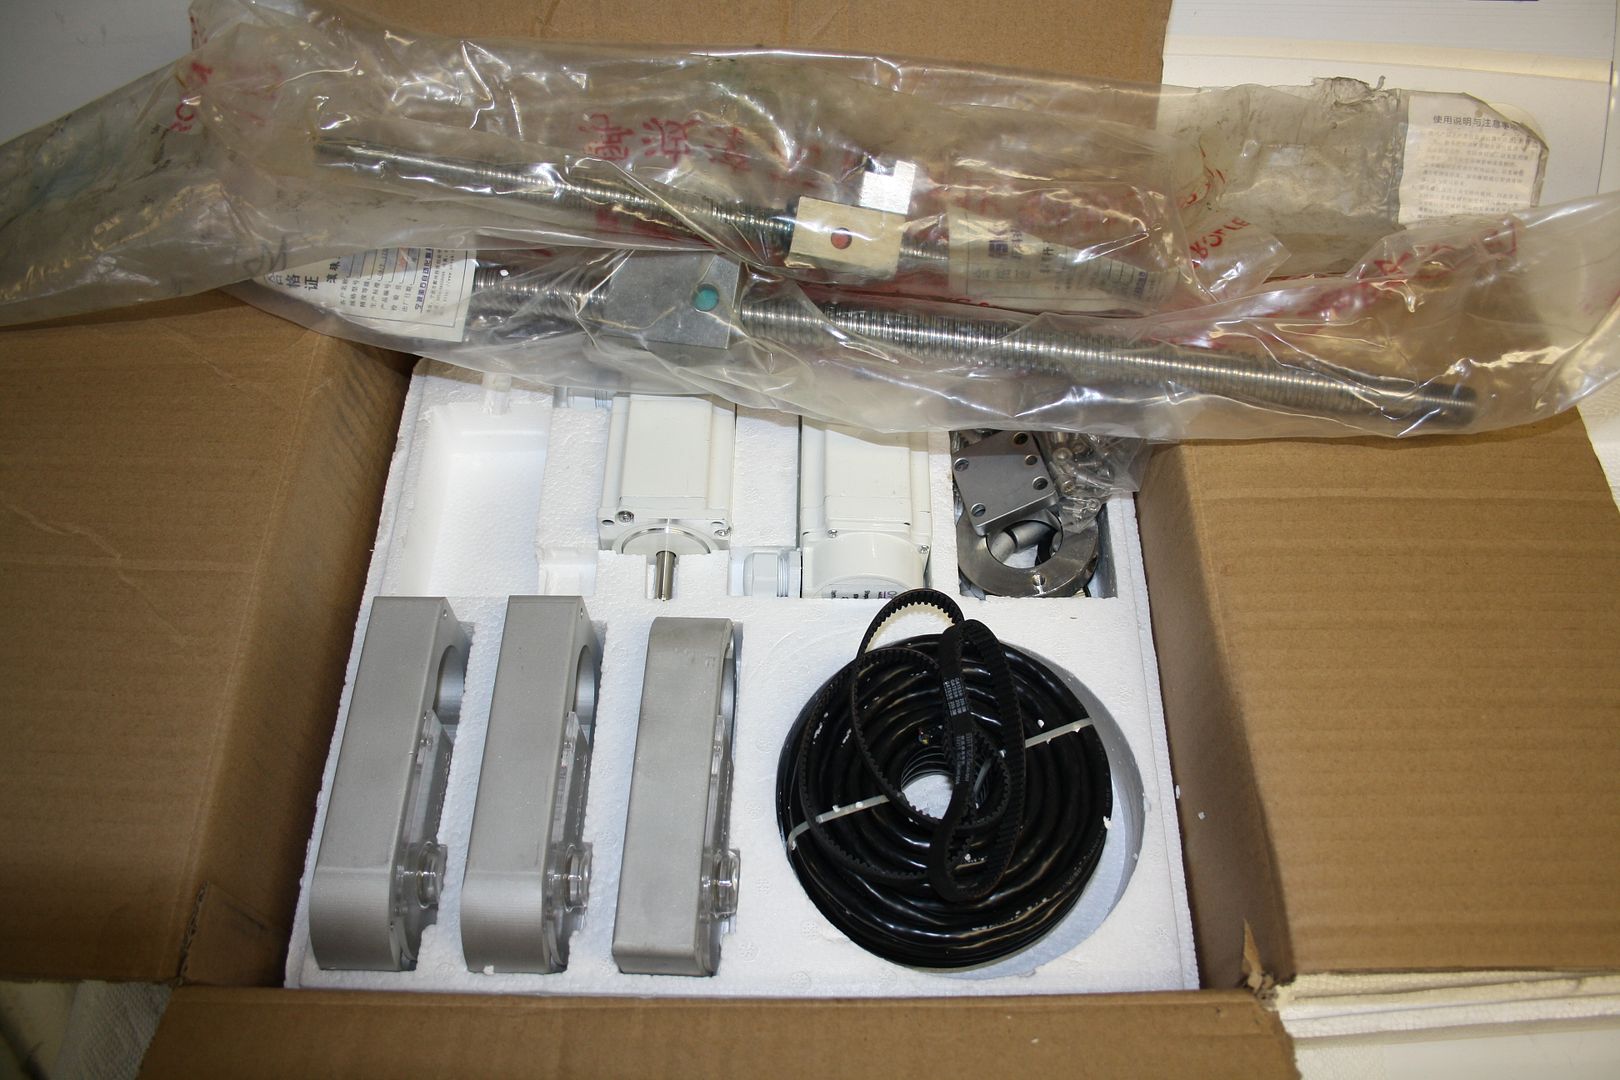
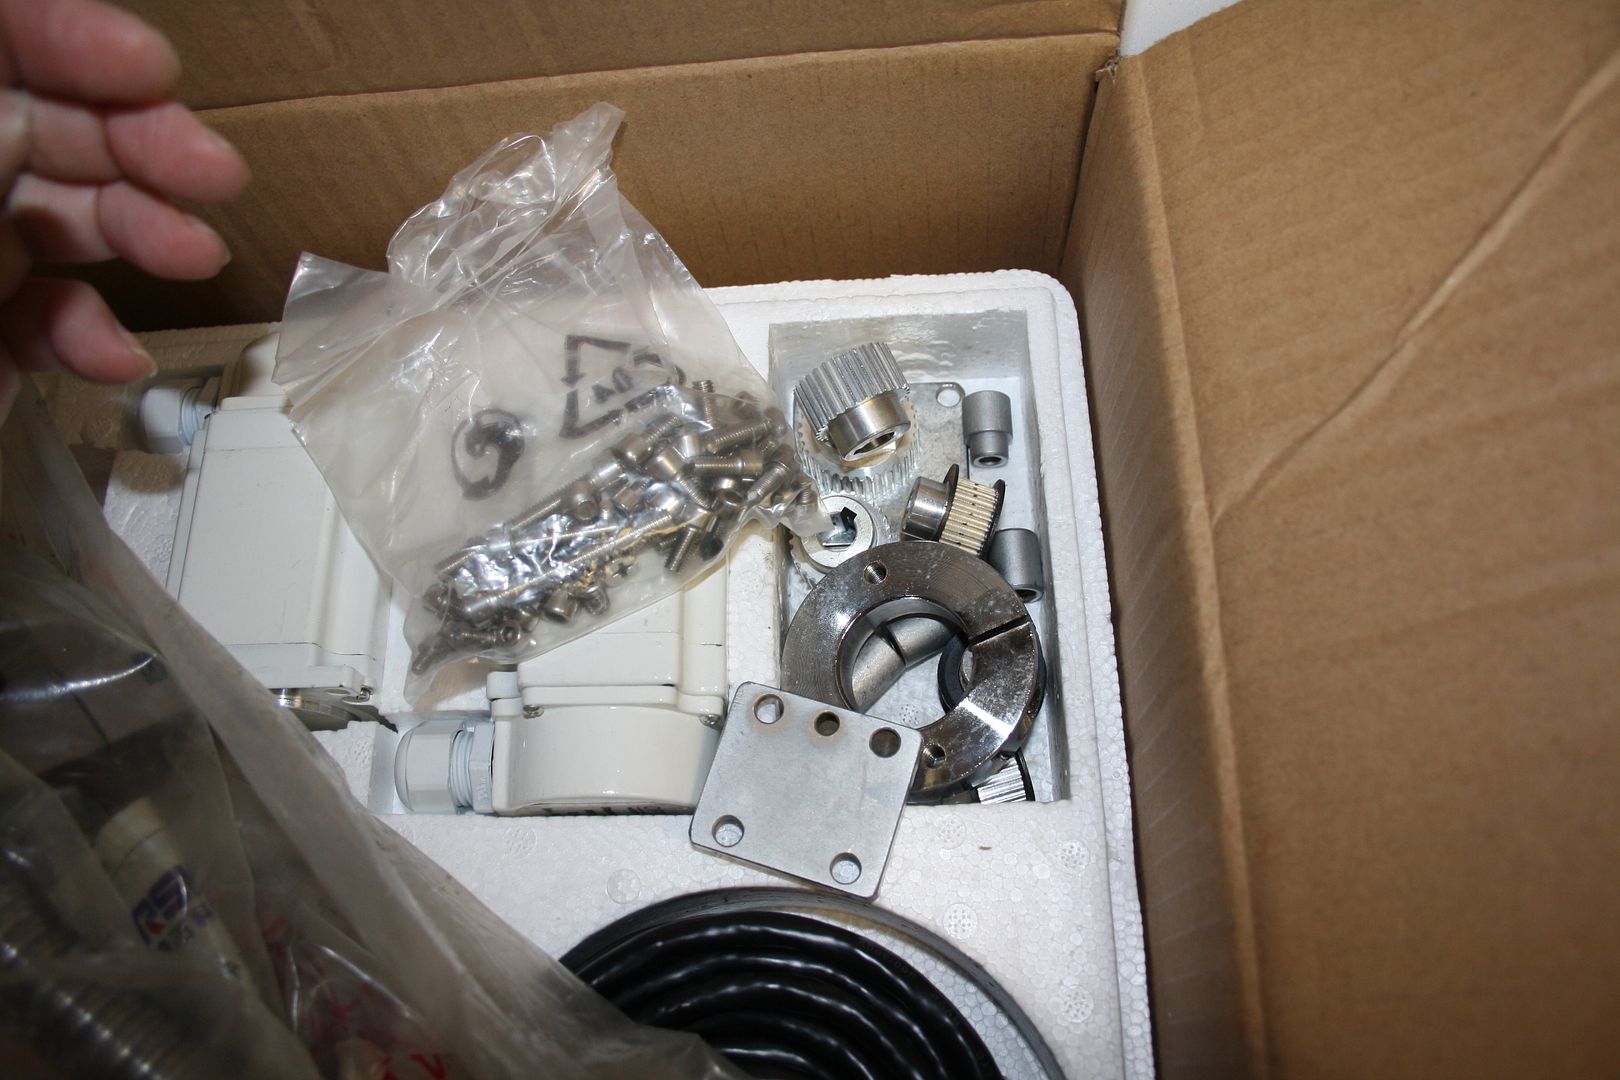
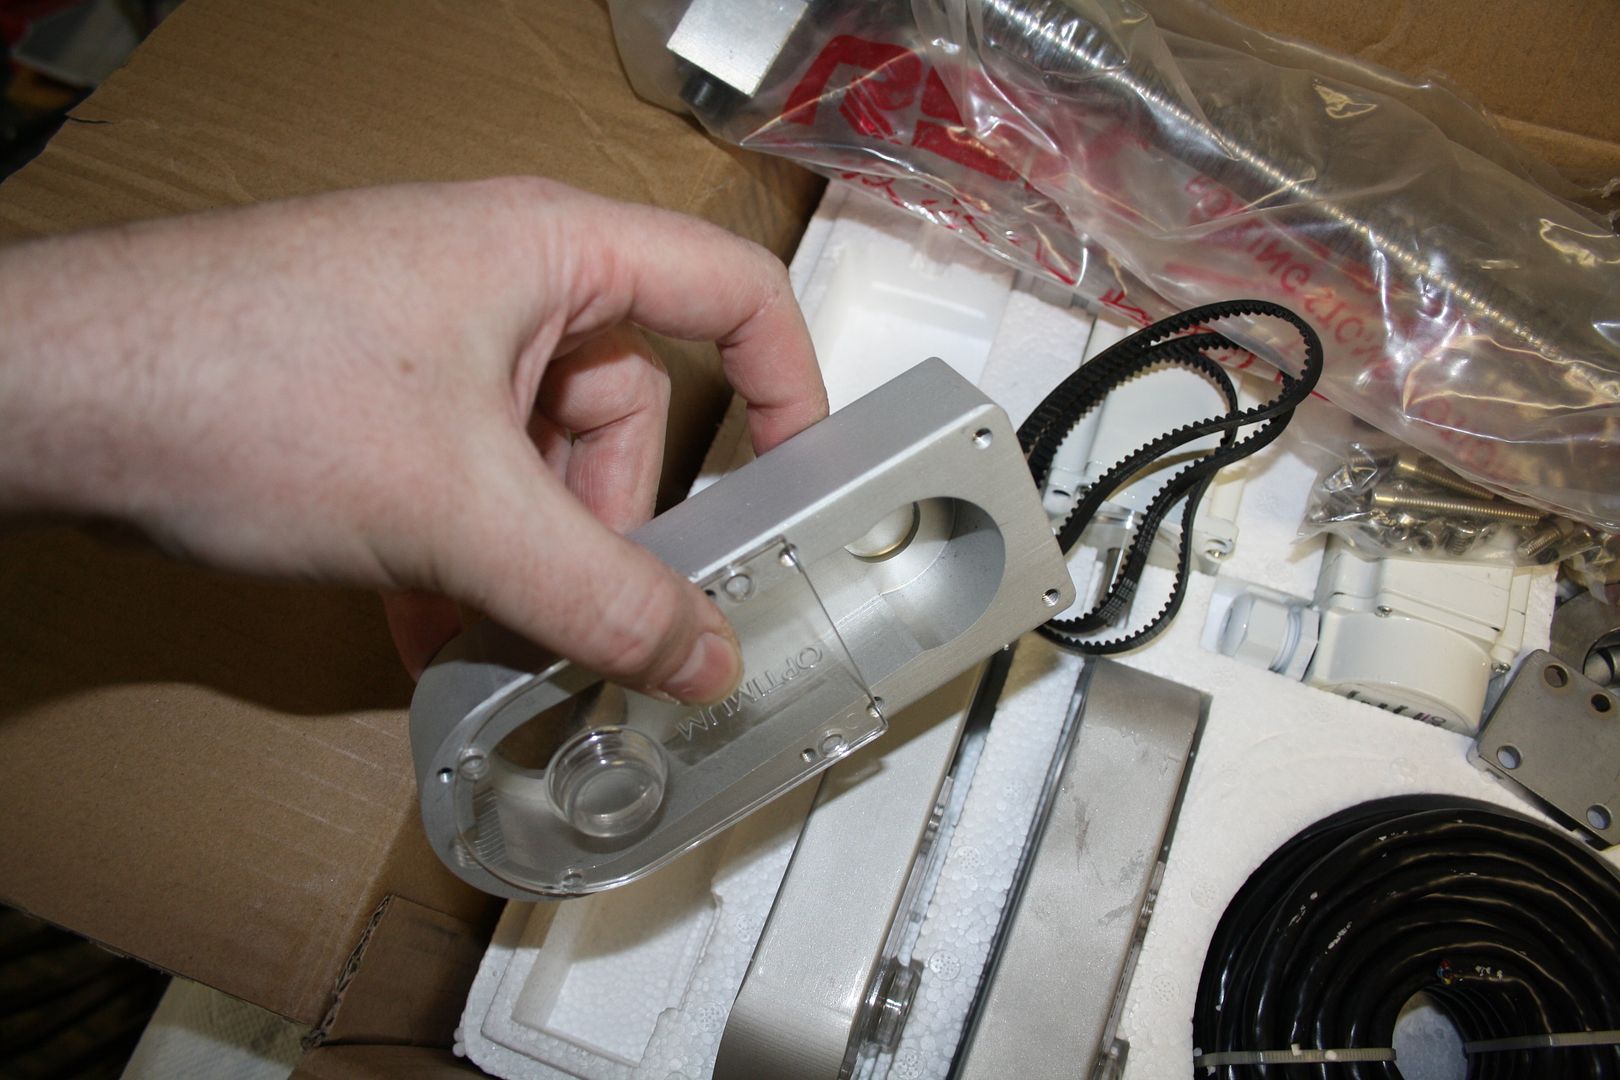
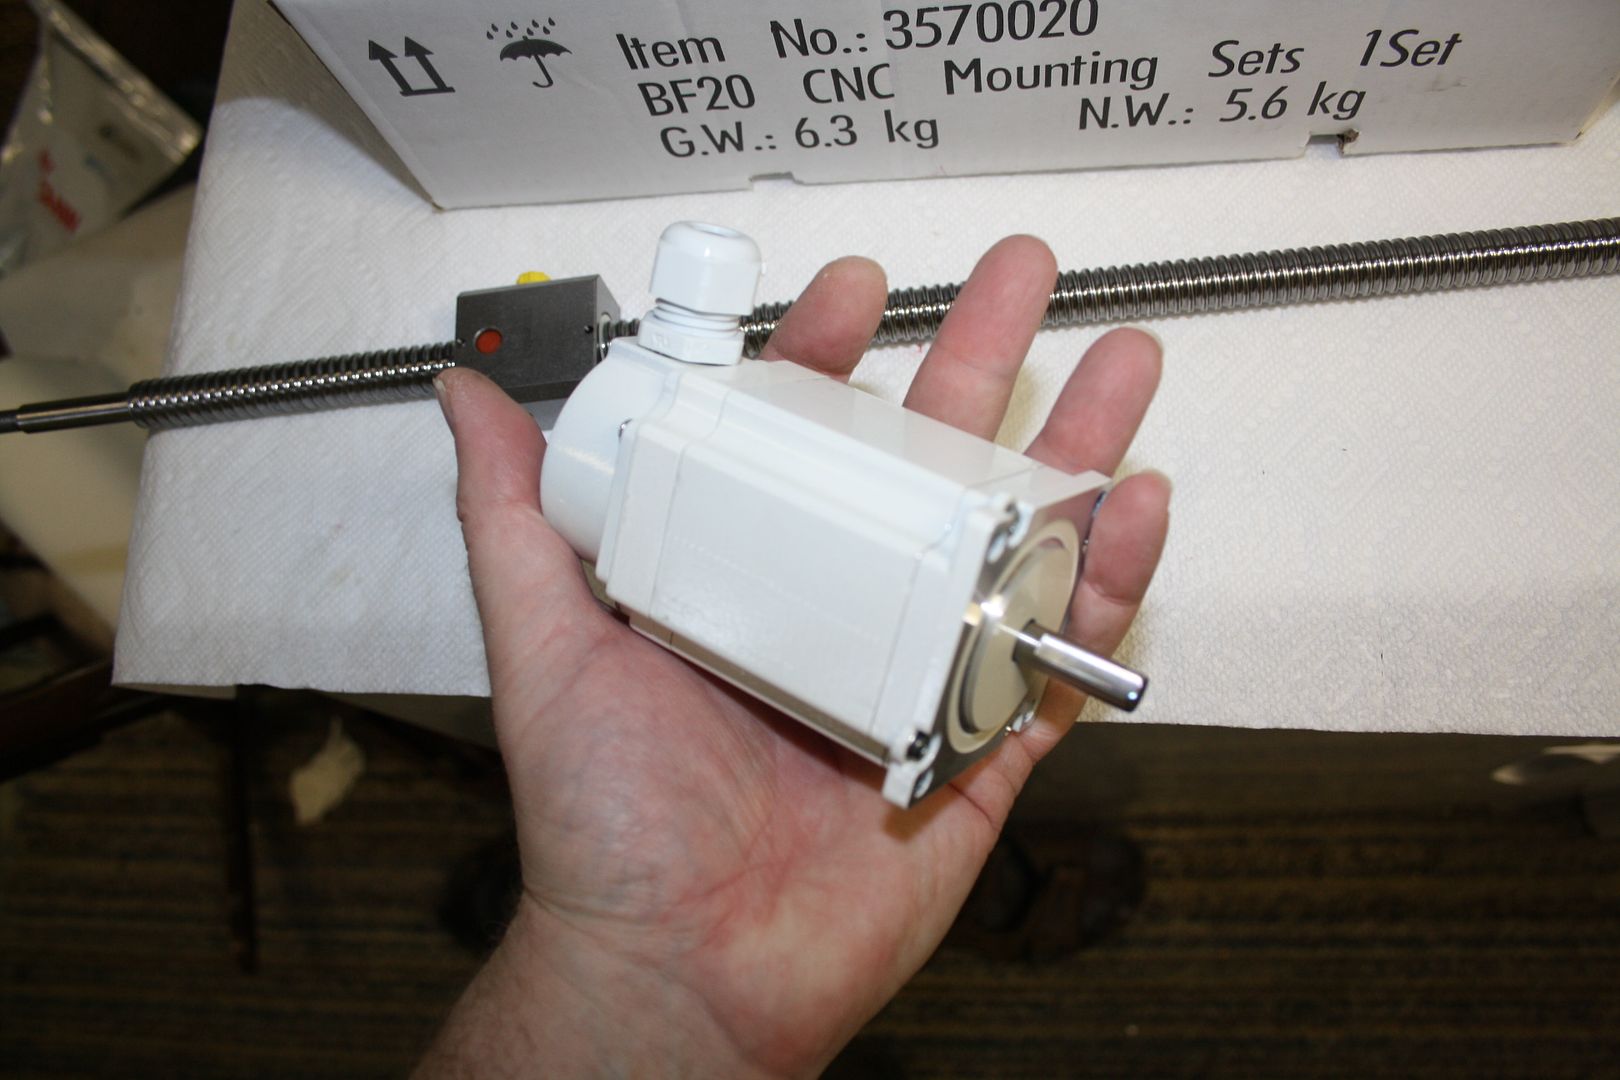

The ball screws are nice and smooth, BIG upgrade from the stock lead screws. Apparently I can even get slightly larger balls and repack the nut for even more precision,... but im not at the advanced stage yet. I'll just be happy to be able to cut 2D parts. :D
-
@Syph007 said:
Well my CNC retrofit kit came today finally! :DNow I just have to figure out how to get it all installed, and pick up a driver board.. flood coolant tank and pump.. and a computer to run it.. learn CAD better.. :D
Hopeful by summer I'll get this all sorted or maybe sooner but its COLD in my shop right now.
The ball screws are nice and smooth, BIG upgrade from the stock lead screws. Apparently I can even get slightly larger balls and repack the nut for even more precision,... but im not at the advanced stage yet. I'll just be happy to be able to cut 2D parts. :D
Now you're good for some serious business!!! Can't wait to see what will come out from your shop in the near future!!!
 :ahhh :ahhh :ahhh :ahhh
-
Looking forward to the what you make with these.
-
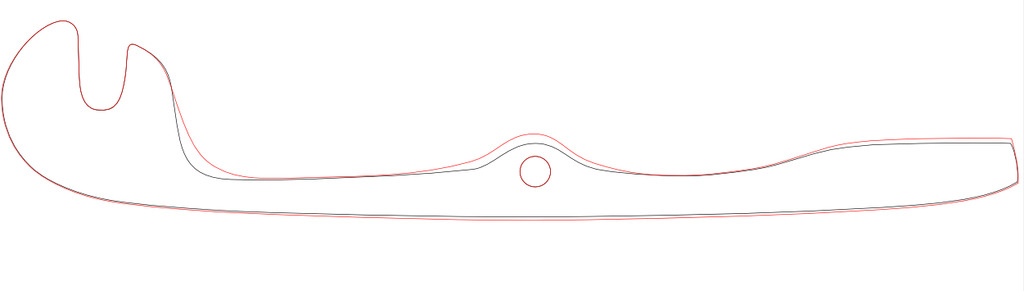
Im down to a critically low amount of scissors backsprings for 93mm alox now, so I forced myself to sit down at the computer and work on a new file. Ver 2.0 of the backspring is pretty much the same, but with some tweaks to make it easier to sand and finish, and also strengthen it.
I was always worried about the strength of the spring over the pivot hole so I beefed that up a bit. I use a 1/2 inch sanding mandrel to finish the inside edges and it could never get into the tight area near then end where the scissors tip rests so I increased that radius. The end of the spring that engages the scissors pivot is also slightly thicker which should give the scissors a bit more snap.
Now I have to wait 3-4 weeks for the waterjet, then heat treat, so hopefully in 2 months I should be restocked.
-
@Syph007 said:
Im down to a critically low amount of scissors backsprings for 93mm alox now, so I forced myself to sit down at the computer and work on a new file. Ver 2.0 of the backspring is pretty much the same, but with some tweaks to make it easier to sand and finish, and also strengthen it.I was always worried about the strength of the spring over the pivot hole so I beefed that up a bit. I use a 1/2 inch sanding mandrel to finish the inside edges and it could never get into the tight area near then end where the scissors tip rests so I increased that radius. The end of the spring that engages the scissors pivot is also slightly thicker which should give the scissors a bit more snap.
Now I have to wait 3-4 weeks for the waterjet, then heat treat, so hopefully in 2 months I should be restocked.
Ever evolving, I like that.

Oh and what happened to the liner lock?

-
-
-
@Syph007 said:
Im down to a critically low amount of scissors backsprings for 93mm alox now, so I forced myself to sit down at the computer and work on a new file. Ver 2.0 of the backspring is pretty much the same, but with some tweaks to make it easier to sand and finish, and also strengthen it.I was always worried about the strength of the spring over the pivot hole so I beefed that up a bit. I use a 1/2 inch sanding mandrel to finish the inside edges and it could never get into the tight area near then end where the scissors tip rests so I increased that radius. The end of the spring that engages the scissors pivot is also slightly thicker which should give the scissors a bit more snap.
Now I have to wait 3-4 weeks for the waterjet, then heat treat, so hopefully in 2 months I should be restocked.
I had a few emails out for quotes and the lowest one I got was actually a local guy about 20 minutes from here. I prefer to use local when I can so Im going over to drop the steel off now. He said 3 weeks. I'm somewhat nervous trying a new shop but if it works out it will be nice to have a local guy I can trust. I would then consider using him to cut a bunch of brass liners out as a next test as cutting them manually... SUCKS! :D
The waterjet pricing is interesting. It works out to somewhere between 3-6 bucks a part, but it depends on how much taper you can accept on the edges. For zero taper its the most expensive as the machine has to go the slowest. Luckily my tolerances are no where near as high as that. For the cheapest cut price it will only have 0.006" of taper over the 0.110" thickness of the steel. That is completely acceptible for me, since I will still need to edge finish anyhow.
Now watch my luck as I get 200 new springs in and Vic decides to kill the 93mm alox liner for 2014...




 I look forward to what you come up with for this


Hello! It looks like you're interested in this conversation, but you don't have an account yet.
Getting fed up of having to scroll through the same posts each visit? When you register for an account, you'll always come back to exactly where you were before, and choose to be notified of new replies (either via email, or push notification). You'll also be able to save bookmarks and upvote posts to show your appreciation to other community members.
With your input, this post could be even better 💗
Register Login


