
EURIKA! Threaded tubes
-
Guess I was wrong again
 I just figured these were the ones after I saw the mods.
-
Although I did find some 2.5 mm threaded ones ;). Ahhhh ohhhhhh. I might let y'all in on it

-
The problem with the body piercing posts is that they are threaded very shallow and it's a problem finding them in the exact length for every tool combination. I find it easier to use the barrel pins. On the spring and backtool pins I use a 4-40 stainless screw that has an unthreaded section near the head. I can trim them to length and pivot the driver or corkscrew on the unthreaded section since they take the most torque. Then I just hide those under the scales.
-
-
Dumb question here, but what exactly is a barrel pin?
It's not dumb if 2 people want to know :)
What are they?I'm pretty sure he's talking about knife pivots like these.
http://www.knifekits.com/vcom/product_info.php?cPath=60_83&products_id=471
-
Dumb question here, but what exactly is a barrel pin?
It's not dumb if 2 people want to know :)
What are they?I'm pretty sure he's talking about knife pivots like these.
http://www.knifekits.com/vcom/product_info.php?cPath=60_83&products_id=471
Yes that's it.
-
Ok, thanks.
-
and
http://www.knifekits.com/vcom/product_info.php?cPath=60_83&products_id=471
has them in 1/2 long which will work up to three tool layers.
-
Well what you can do is put two together with 2-56 threaded rod. Then you have an inch to use. I wouldn't use any longer than that. Also I would try to make sure the joint is in-between a tool not a spring.
-
I found a el cheapo tool that has 2.5 mm barrel bolts or pivot pins. I'm planning on trying them soon so I'll let everyone know how it works out.
-
@tattoosteve99 said:
Well what you can do is put two together with 2-56 threaded rod. Then you have an inch to use. I wouldn't use any longer than that. Also I would try to make sure the joint is in-between a tool not a spring.What he said. I cut the head off a 1/4" long 2-56 screw and screwed two posts together after running them in the drill press into a coarse wetstone to make sure the ends were square and flat. Then I put them together with red locktight and trim to length and make sure the seam is in the middle of your thickest tool. 1/8" barrel pins are easy to work on since they slip right into a Dremel collet. I find the trouble to drill the tools out is far less than the trouble of trying to get 2.5mm hardware.
-
Well what you can do is put two together with 2-56 threaded rod. Then you have an inch to use. I wouldn't use any longer than that. Also I would try to make sure the joint is in-between a tool not a spring.
What he said. I cut the head off a 1/4" long 2-56 screw and screwed two posts together after running them in the drill press into a coarse wetstone to make sure the ends were square and flat. Then I put them together with red locktight and trim to length and make sure the seam is in the middle of your thickest tool. 1/8" barrel pins are easy to work on since they slip right into a Dremel collet. I find the trouble to drill the tools out is far less than the trouble of trying to get 2.5mm hardware.
I like your solution since you can use ready made parts. The only downside is though that those parts are now only good for that type of sak since the holes are drilled out. Have you thought about getting 3 mm stainless steel rod and drilling/tapping that for a similar solution? That was one of the reasons I wanted a mini lathe for, was to center drill the rod.
-
I have designed my own sex bolts and I'll have around 200 of them run off at emachineshop.com when I have $400 to spare. I'm sticking with 1/8" because 2-56 screws are the lower limit for strength, any smaller with the screws and I wouldn't trust them. 3mm doesn't leave much to drill and thread.
Some people wonder why it takes me so long to do what I do. The biggest reason is that for every step, every part and every process I try so many different things to see what's the best way to make them at a decent pace and then I work on outsource the busywork so I can focus on finishing everything perfectly. I have poured over this threaded pin issue more than anyone, trust me. There are limitations that I have settled on to make what I can make better such as 4 layer maximum and no slots for standard T&T . A long series of compromises that fits in your pocket.. or something like that.
-
Well what you can do is put two together with 2-56 threaded rod. Then you have an inch to use. I wouldn't use any longer than that. Also I would try to make sure the joint is in-between a tool not a spring.
What he said. I cut the head off a 1/4" long 2-56 screw and screwed two posts together after running them in the drill press into a coarse wetstone to make sure the ends were square and flat. Then I put them together with red locktight and trim to length and make sure the seam is in the middle of your thickest tool. 1/8" barrel pins are easy to work on since they slip right into a Dremel collet. I find the trouble to drill the tools out is far less than the trouble of trying to get 2.5mm hardware.
I like your solution since you can use ready made parts. The only downside is though that those parts are now only good for that type of sak since the holes are drilled out. Have you thought about getting 3 mm stainless steel rod and drilling/tapping that for a similar solution? That was one of the reasons I wanted a mini lathe for, was to center drill the rod.
And I don't mean to discourage you from trying to drill out some 3mm rod but depending on the material you use you could drive yourself crazy trying to run a .059 bit through it while staying on center and then getting a fragile little 2-56 tap through it without something invariably going off center or snapping off. There's a reason the barrel pins I use stop at 1/2" length, that's the limit for tap depth at that diameter. Tiny precision drilling and tapping like that has to be done on very precise machinery and you may be disappointed with what a benchtop mini-lathe can accomplish.
I haven't worked in a real machine shop for years so I could just be making wrong assumptions based on how it used to be. Maybe someone with much more knowledge of current machining processes like Jsews would tell you different.
-
Well what you can do is put two together with 2-56 threaded rod. Then you have an inch to use. I wouldn't use any longer than that. Also I would try to make sure the joint is in-between a tool not a spring.
What he said. I cut the head off a 1/4" long 2-56 screw and screwed two posts together after running them in the drill press into a coarse wetstone to make sure the ends were square and flat. Then I put them together with red locktight and trim to length and make sure the seam is in the middle of your thickest tool. 1/8" barrel pins are easy to work on since they slip right into a Dremel collet. I find the trouble to drill the tools out is far less than the trouble of trying to get 2.5mm hardware.
I like your solution since you can use ready made parts. The only downside is though that those parts are now only good for that type of sak since the holes are drilled out. Have you thought about getting 3 mm stainless steel rod and drilling/tapping that for a similar solution? That was one of the reasons I wanted a mini lathe for, was to center drill the rod.
And I don't mean to discourage you from trying to drill out some 3mm rod but depending on the material you use you could drive yourself crazy trying to run a .059 bit through it while staying on center and then getting a fragile little 2-56 tap through it without something invariably going off center or snapping off. There's a reason the barrel pins I use stop at 1/2" length, that's the limit for tap depth at that diameter. Tiny precision drilling and tapping like that has to be done on very precise machinery and you may be disappointed with what a benchtop mini-lathe can accomplish.
I haven't worked in a real machine shop for years so I could just be making wrong assumptions based on how it used to be. Maybe someone with much more knowledge of current machining processes like Jsews would tell you different.
Oh I know how irritating small taps are. I worked in a lab where we build our own instruments. I had to make electron gun lenses out of stainless 310. The parts were small and I had to tap small holes to connect electical wires. It was aweful, I had to remake parts that I broke taps off in.
The threaded tube though, im not wanting to make it drilled all the way through, i dont see why i would need to. Just drilled 1/4 inch into each end, or would I need more thread than that to hold a screw? Thats what my plan is anyhow.
-
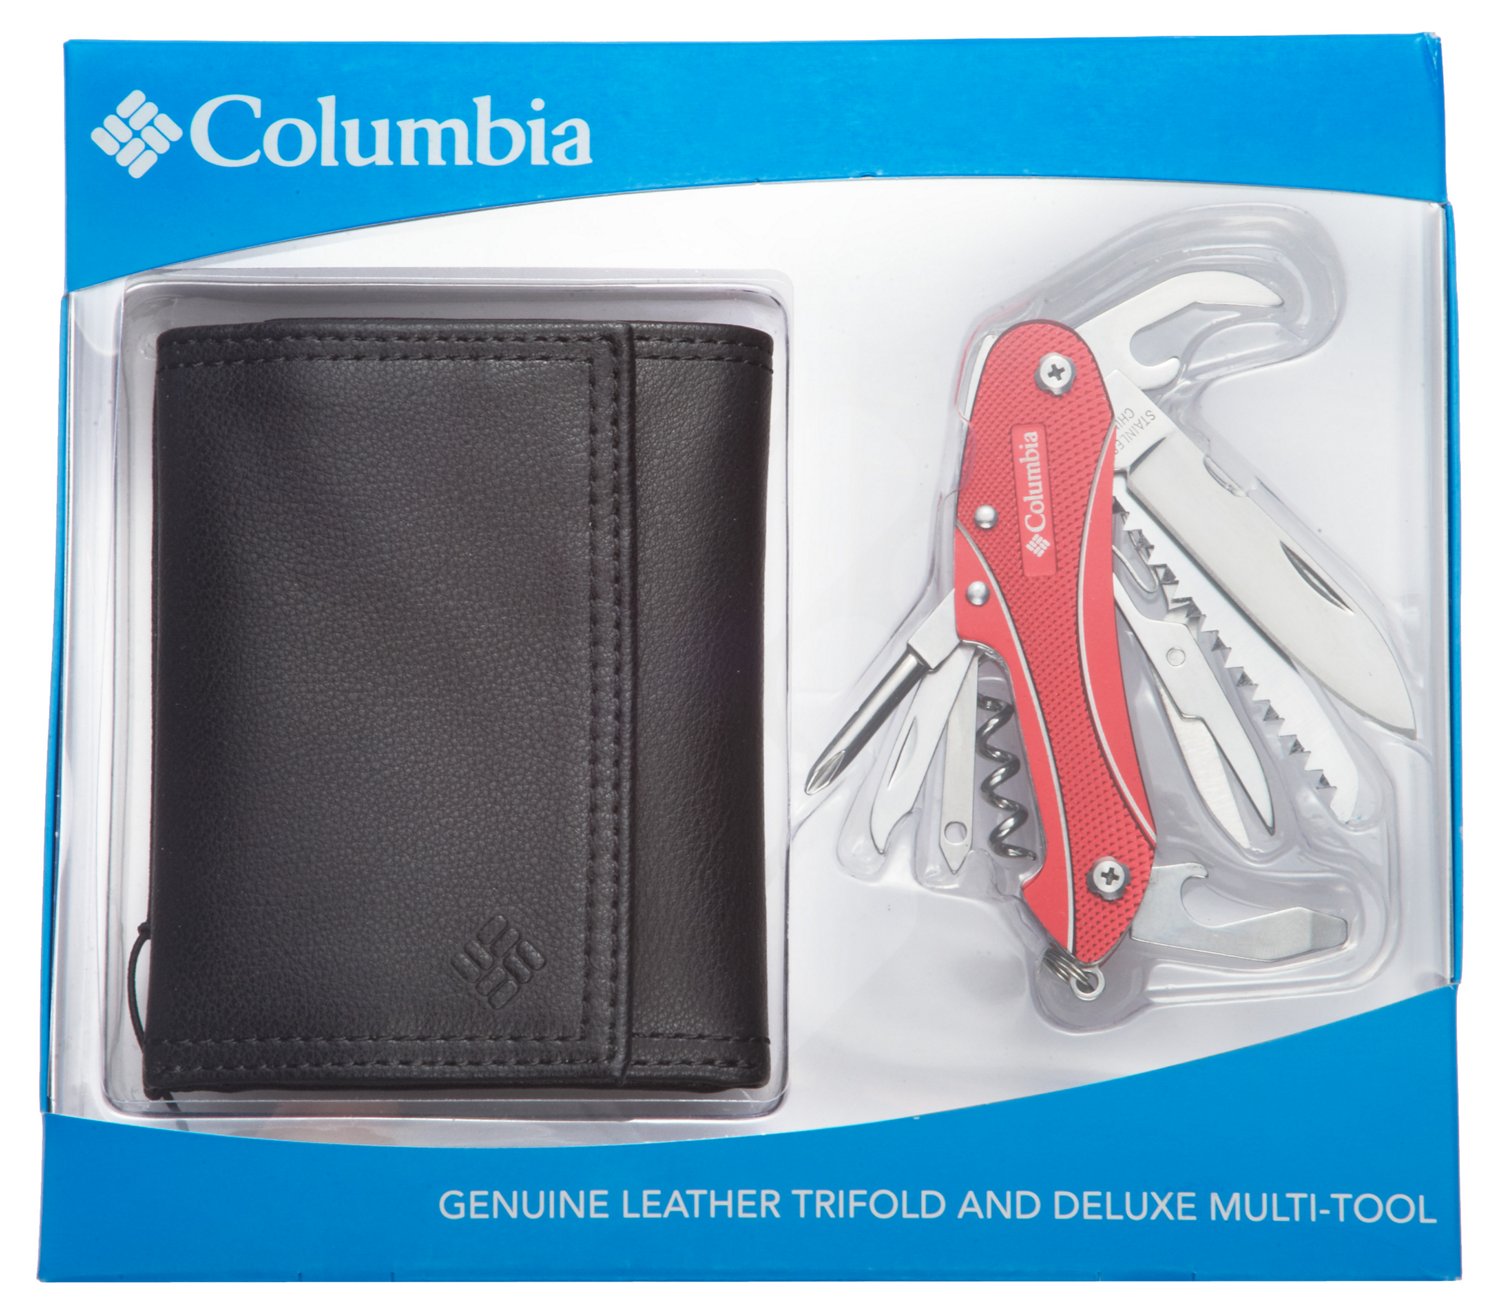
I'm trying to find a pic to a tool that has the 2.5mm barrel bolts. Can't seem to locate one. It's a elcheapo tool, Columbia SAK type knife with screws in it. There measure right at 2.5mm.
-
@tattoosteve99 said:
I'm trying to find a pic to a tool that has the 2.5mm barrel bolts. Can't seem to locate one. It's a elcheapo tool, Columbia SAK type knife with screws in it. There measure right at 2.5mm.Is it perhaps something like this?

or this?



Hello! It looks like you're interested in this conversation, but you don't have an account yet.
Getting fed up of having to scroll through the same posts each visit? When you register for an account, you'll always come back to exactly where you were before, and choose to be notified of new replies (either via email, or push notification). You'll also be able to save bookmarks and upvote posts to show your appreciation to other community members.
With your input, this post could be even better 💗
Register Login


